Read page text
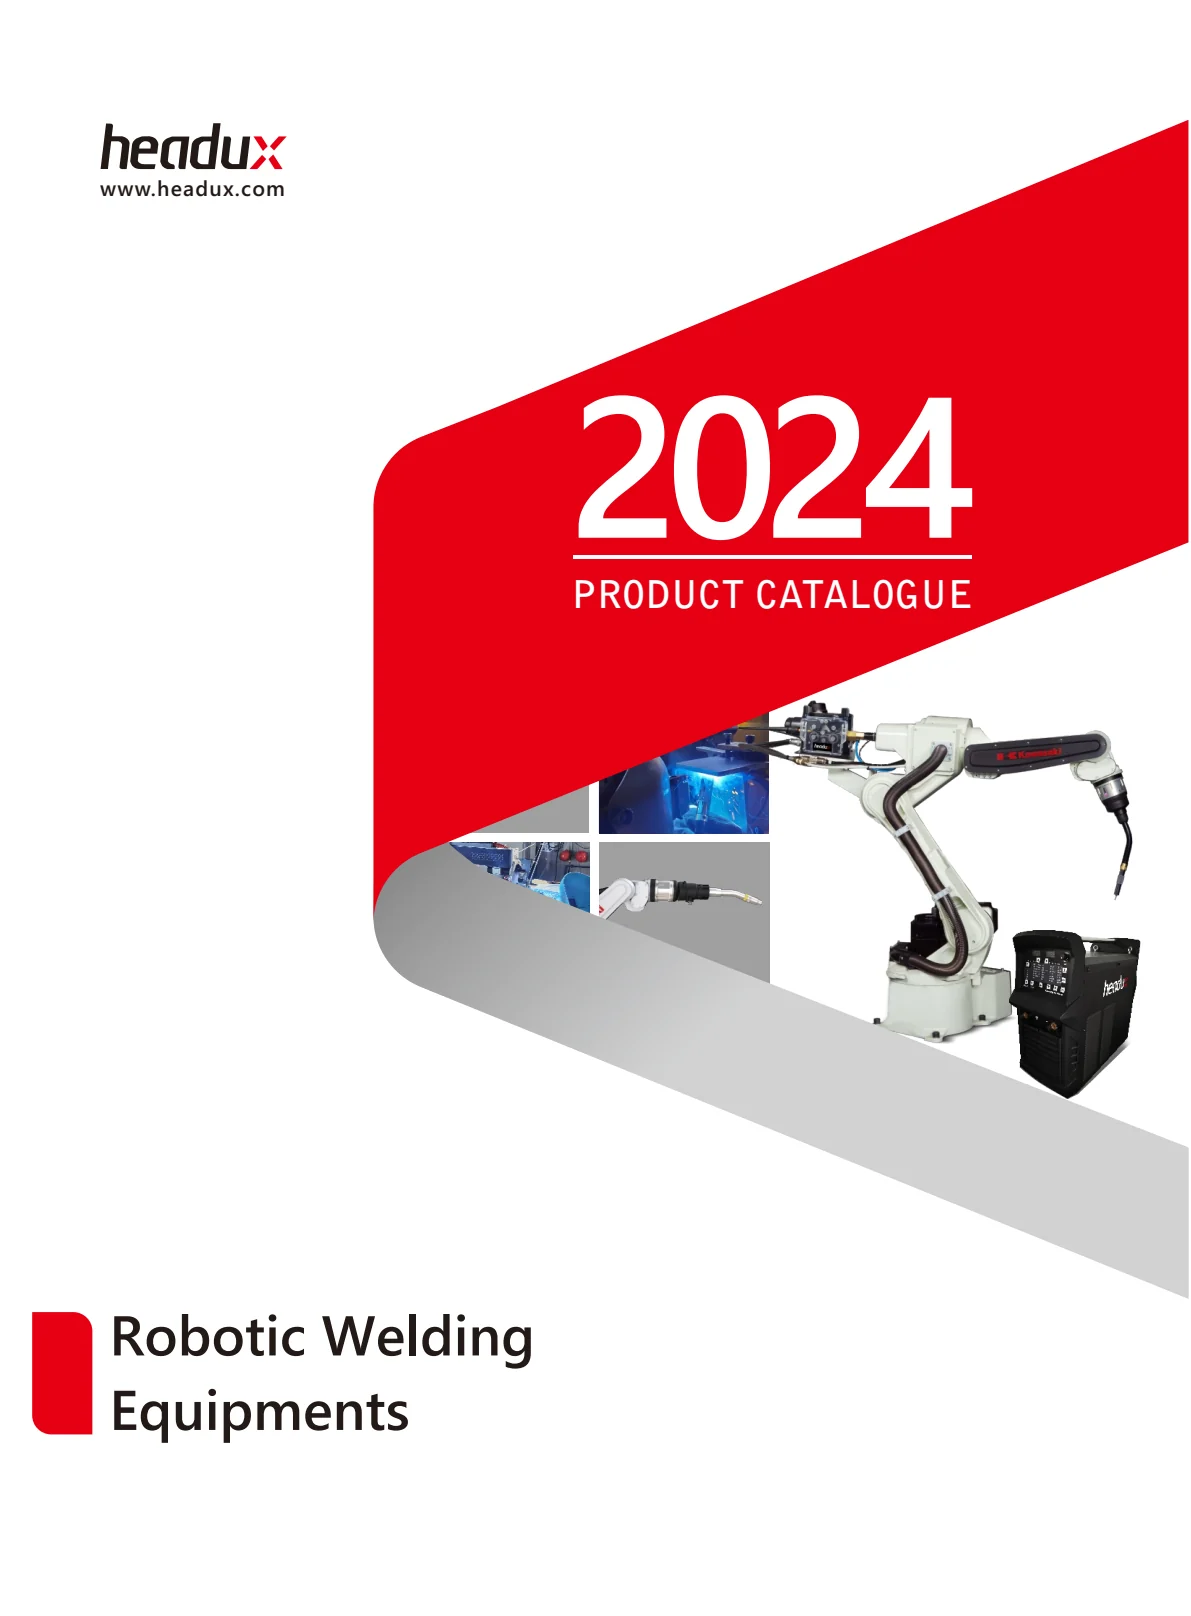
Robotic Welding Equipments www.headux.com PRODUCT CATALOGUE 2024
Read page text
About Headux TitanMig 350/500R TitanMig 350RL TitanMig 350RS TitanMig X4/X5R Pulse X-Super MIG Welding Process 1 3 5 7 9 11 INSPIRED BY POWER
Read page text
About Headux TitanMig 350/500R TitanMig 350RL TitanMig 350RS TitanMig X4/X5R Pulse X-Super MIG Welding Process 1 3 5 7 9 11 INSPIRED BY POWER
Read page text
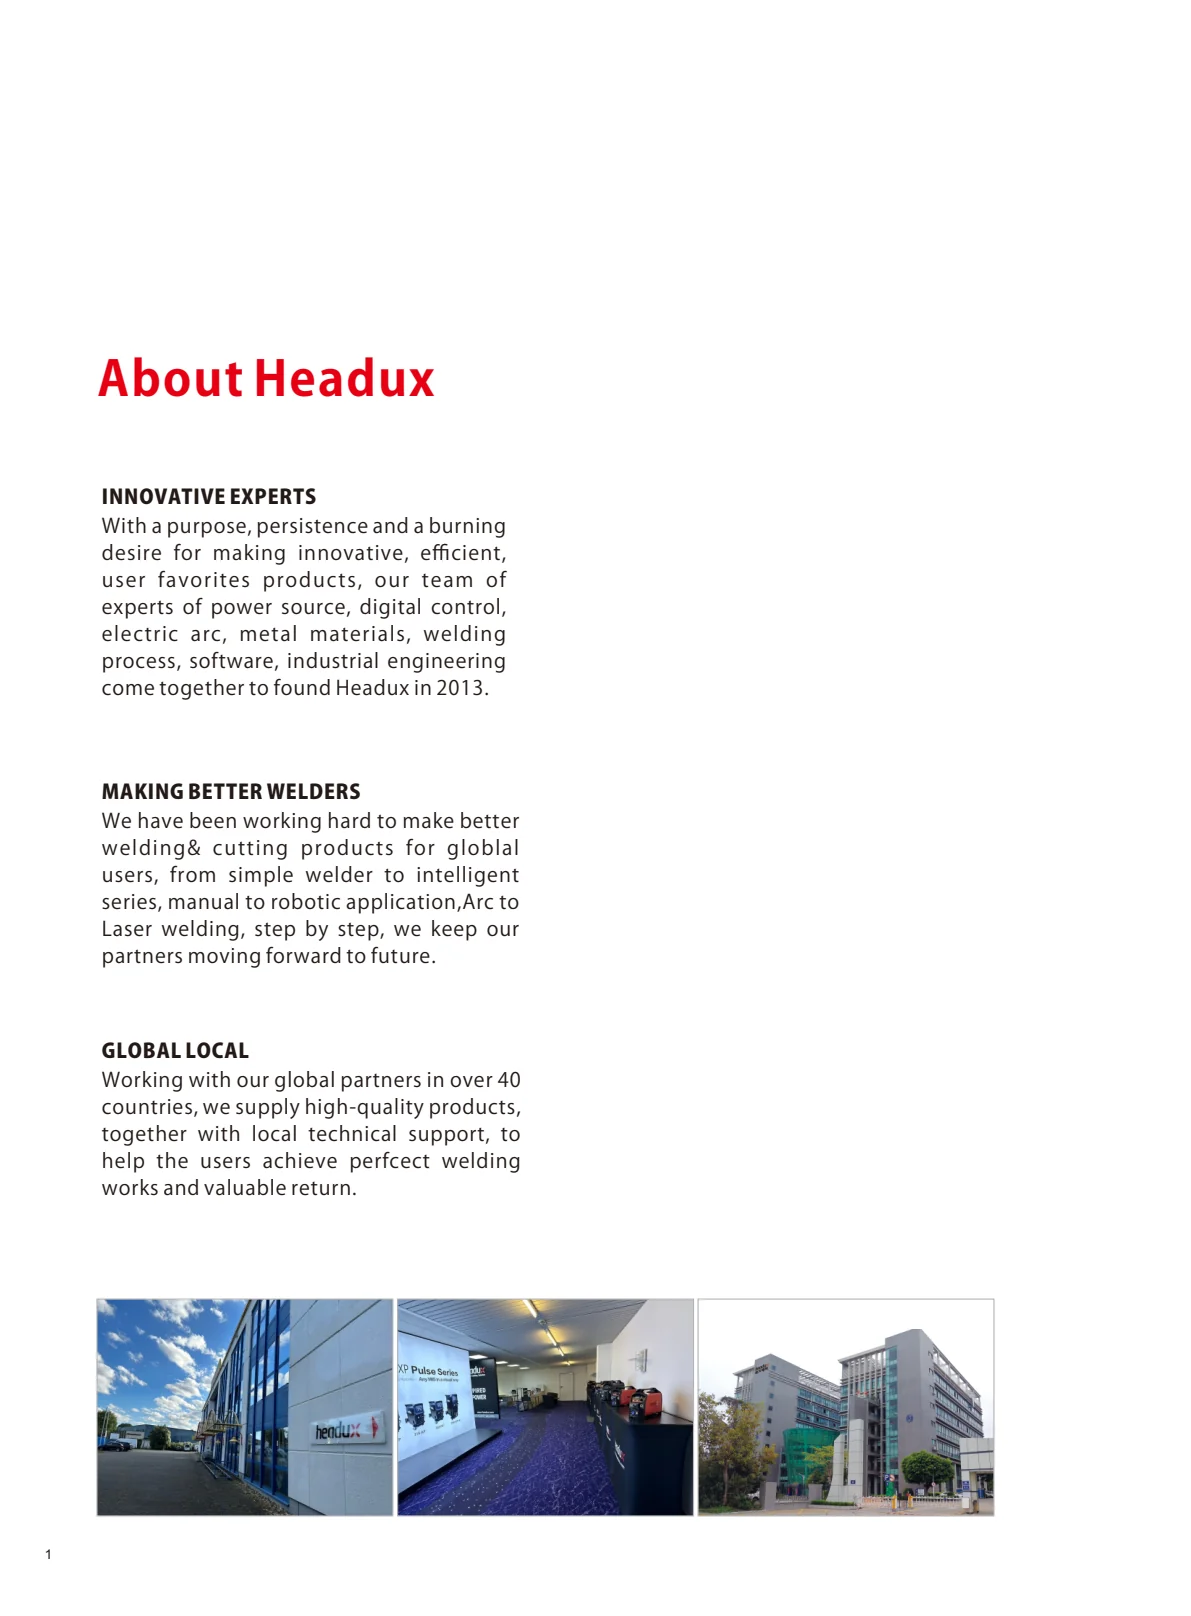
1 2 MAKING BETTER WELDERS We have been working hard to make better welding& cutting products for globlal users, from simple welder to intelligent series, manual to robotic application,Arc to Laser welding, step by step, we keep our partners moving forward to future. GLOBAL LOCAL Working with our global partners in over 40 countries, we supply high-quality products, together with local technical support, to help the users achieve perfcect welding works and valuable return. INNOVATIVE EXPERTS With a purpose, persistence and a burning desire for making innovative, efficient, user favorites products, our team of experts of power source, digital control, electric arc, metal materials, welding process, software, industrial engineering come together to found Headux in 2013. About Headux
Read page text
1 2 MAKING BETTER WELDERS We have been working hard to make better welding& cutting products for globlal users, from simple welder to intelligent series, manual to robotic application,Arc to Laser welding, step by step, we keep our partners moving forward to future. GLOBAL LOCAL Working with our global partners in over 40 countries, we supply high-quality products, together with local technical support, to help the users achieve perfcect welding works and valuable return. INNOVATIVE EXPERTS With a purpose, persistence and a burning desire for making innovative, efficient, user favorites products, our team of experts of power source, digital control, electric arc, metal materials, welding process, software, industrial engineering come together to found Headux in 2013. About Headux
Read page text
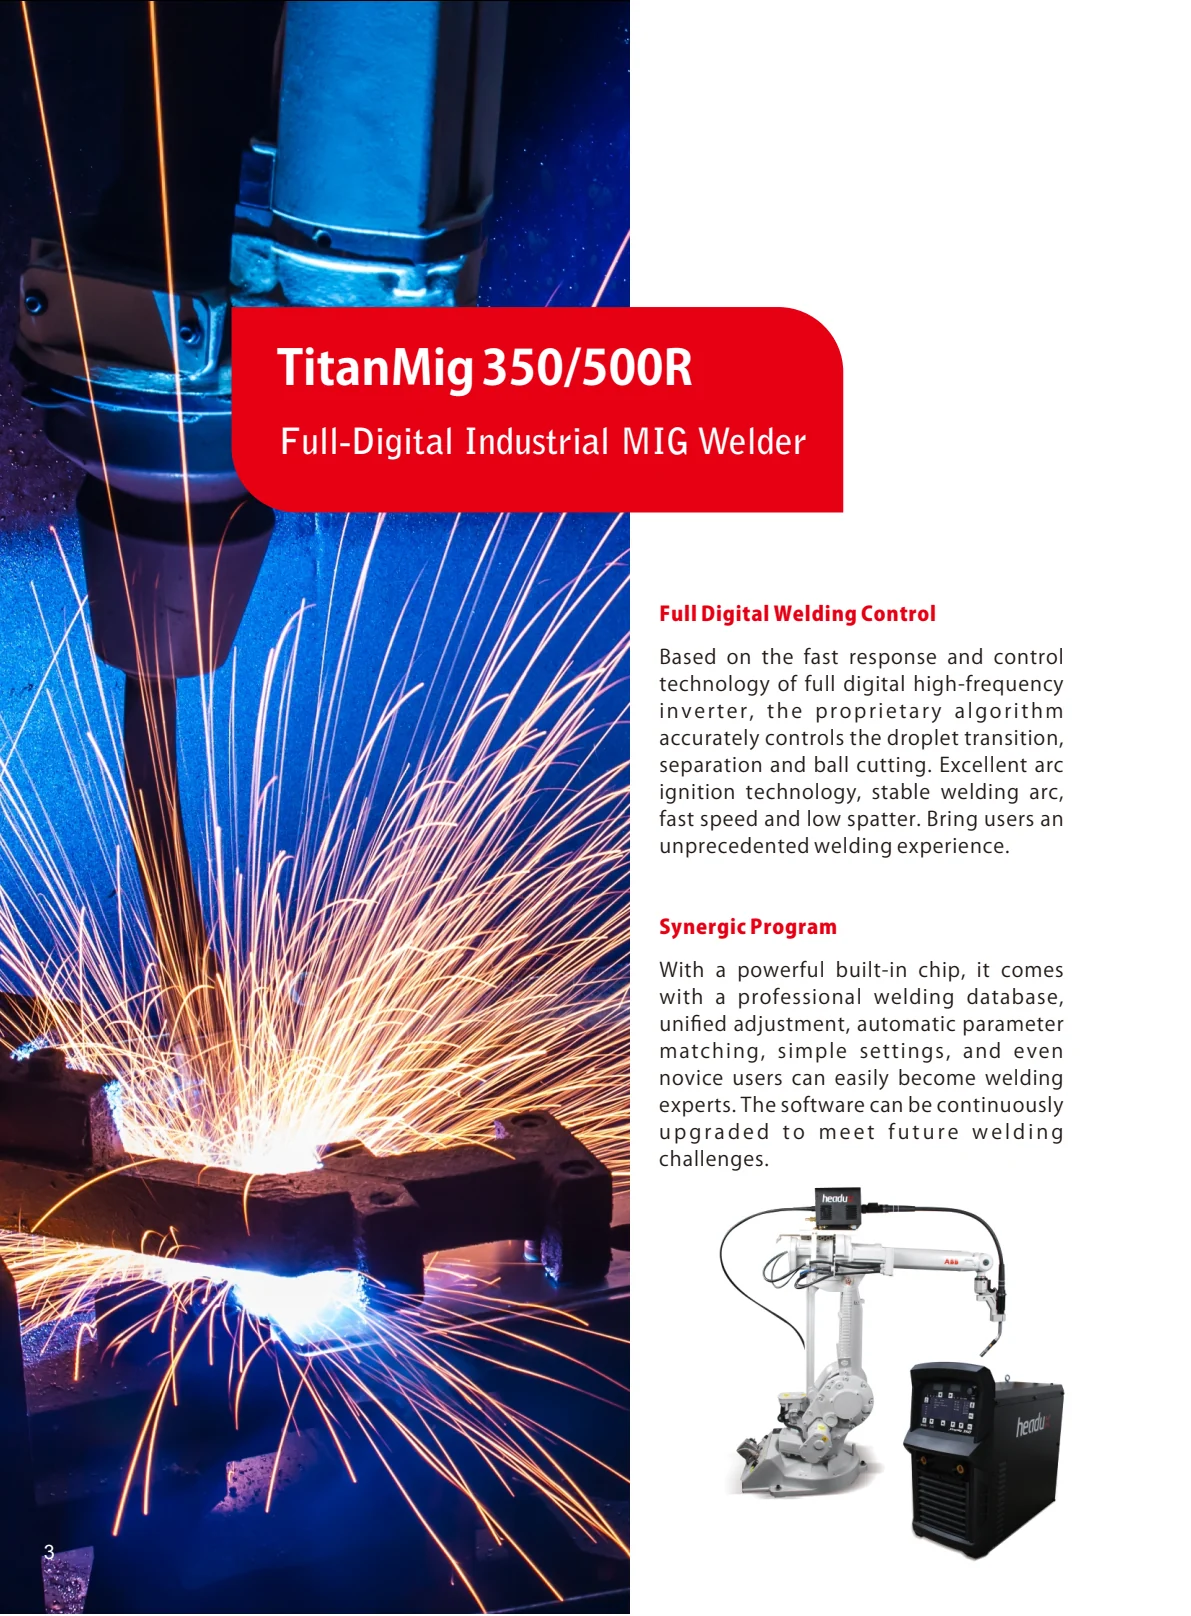
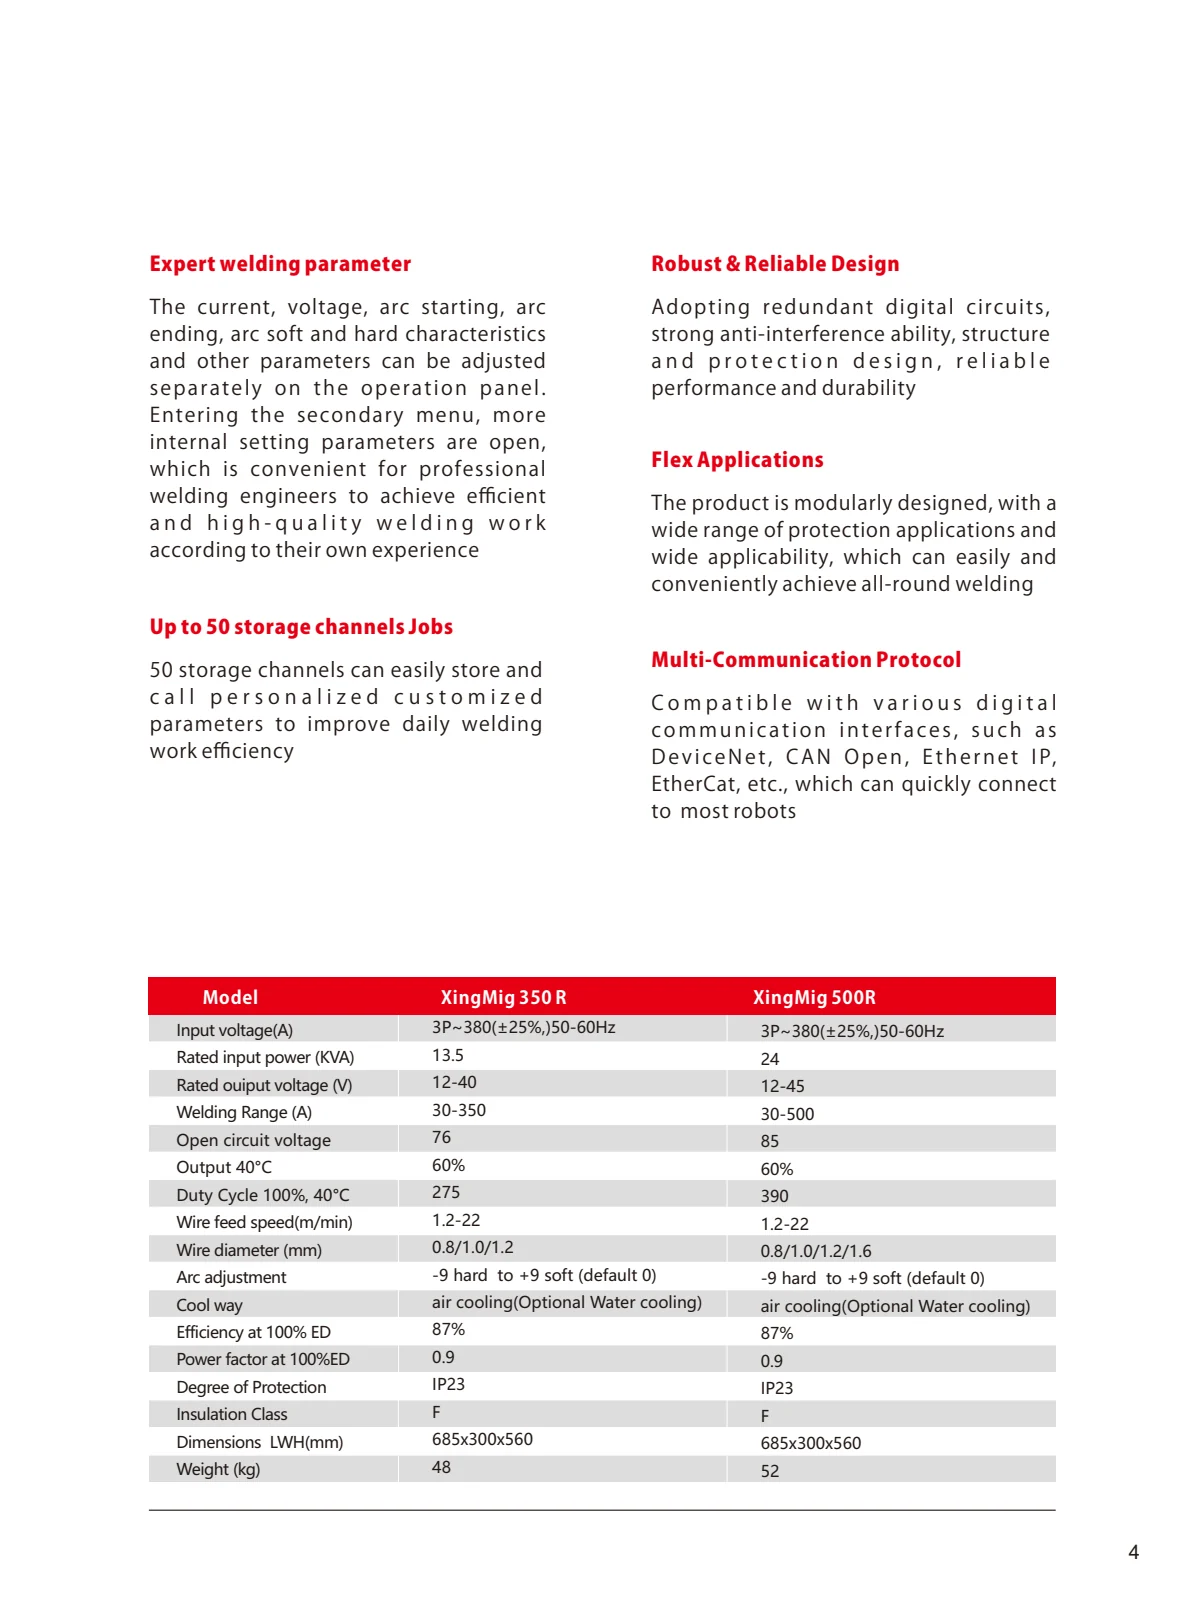
TitanMig 350/500R 3P~380(±25%,)50-60Hz 13.5 12-40 30-350 76 60% 275 1.2-22 0.8/1.0/1.2 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 48 Input voltage(A) Rated input power (KVA) Rated ouiput voltage (V) Welding Range (A) Open circuit voltage Output 40°C Duty Cycle 100%, 40°C Wire feed speed(m/min) Wire diameter (mm) Arc adjustment Cool way Efficiency at 100% ED Power factor at 100%ED Degree of Protection Insulation Class Dimensions LWH(mm) Weight (kg) Model XingMig 350 R XingMig 500R 3 4 Full Digital Welding Control Based on the fast response and control technology of full digital high-frequency i n v e r t e r , t h e p r o p r i e t a r y a l g o r i t h m accurately controls the droplet transition, separation and ball cutting. Excellent arc ignition technology, stable welding arc, fast speed and low spatter. Bring users an unprecedented welding experience. Synergic Program With a powerful built-in chip, it comes with a professional welding database, unified adjustment, automatic parameter matching, simple settings, and even novice users can easily become welding experts. The software can be continuously u p g r a d e d t o m e e t f u t u r e w e l d i n g challenges. Expert welding parameter The current, voltage, arc starting, arc ending, arc soft and hard characteristics and other parameters can be adjusted s e p a r a t e l y o n t h e o p e r a t i o n p a n e l . Entering the secondary menu, more internal setting parameters are open, which is convenient for professional welding engineers to achieve efficient a n d h i g h - q u a l i t y w e l d i n g w o r k according to their own experience Up to 50 storage channels Jobs 50 storage channels can easily store and c a l l p e r s o n a l i z e d c u s t o m i z e d parameters to improve daily welding work efficiency Flex Applications The product is modularly designed, with a wide range of protection applications and wide applicability, which can easily and conveniently achieve all-round welding Multi-Communication Protocol C o m p a t i b l e w i t h v a r i o u s d i g i t a l c o m m u n i c a t i o n i n t e r f a c e s , s u c h a s D e v i c e N e t , C A N O p e n , E t h e r n e t I P, EtherCat, etc., which can quickly connect to most robots Robust & Reliable Design Adopting redundant digital circuits, strong anti-interference ability, structure a n d p r o t e c t i o n d e s i g n , r e l i a b l e performance and durability Full-Digital Industrial MIG Welder 3P~380(±25%,)50-60Hz 24 12-45 30-500 85 60% 390 1.2-22 0.8/1.0/1.2/1.6 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 52
Read page text
TitanMig 350/500R 3P~380(±25%,)50-60Hz 13.5 12-40 30-350 76 60% 275 1.2-22 0.8/1.0/1.2 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 48 Input voltage(A) Rated input power (KVA) Rated ouiput voltage (V) Welding Range (A) Open circuit voltage Output 40°C Duty Cycle 100%, 40°C Wire feed speed(m/min) Wire diameter (mm) Arc adjustment Cool way Efficiency at 100% ED Power factor at 100%ED Degree of Protection Insulation Class Dimensions LWH(mm) Weight (kg) Model XingMig 350 R XingMig 500R 3 4 Full Digital Welding Control Based on the fast response and control technology of full digital high-frequency i n v e r t e r , t h e p r o p r i e t a r y a l g o r i t h m accurately controls the droplet transition, separation and ball cutting. Excellent arc ignition technology, stable welding arc, fast speed and low spatter. Bring users an unprecedented welding experience. Synergic Program With a powerful built-in chip, it comes with a professional welding database, unified adjustment, automatic parameter matching, simple settings, and even novice users can easily become welding experts. The software can be continuously u p g r a d e d t o m e e t f u t u r e w e l d i n g challenges. Expert welding parameter The current, voltage, arc starting, arc ending, arc soft and hard characteristics and other parameters can be adjusted s e p a r a t e l y o n t h e o p e r a t i o n p a n e l . Entering the secondary menu, more internal setting parameters are open, which is convenient for professional welding engineers to achieve efficient a n d h i g h - q u a l i t y w e l d i n g w o r k according to their own experience Up to 50 storage channels Jobs 50 storage channels can easily store and c a l l p e r s o n a l i z e d c u s t o m i z e d parameters to improve daily welding work efficiency Flex Applications The product is modularly designed, with a wide range of protection applications and wide applicability, which can easily and conveniently achieve all-round welding Multi-Communication Protocol C o m p a t i b l e w i t h v a r i o u s d i g i t a l c o m m u n i c a t i o n i n t e r f a c e s , s u c h a s D e v i c e N e t , C A N O p e n , E t h e r n e t I P, EtherCat, etc., which can quickly connect to most robots Robust & Reliable Design Adopting redundant digital circuits, strong anti-interference ability, structure a n d p r o t e c t i o n d e s i g n , r e l i a b l e performance and durability Full-Digital Industrial MIG Welder 3P~380(±25%,)50-60Hz 24 12-45 30-500 85 60% 390 1.2-22 0.8/1.0/1.2/1.6 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 52
Read page text
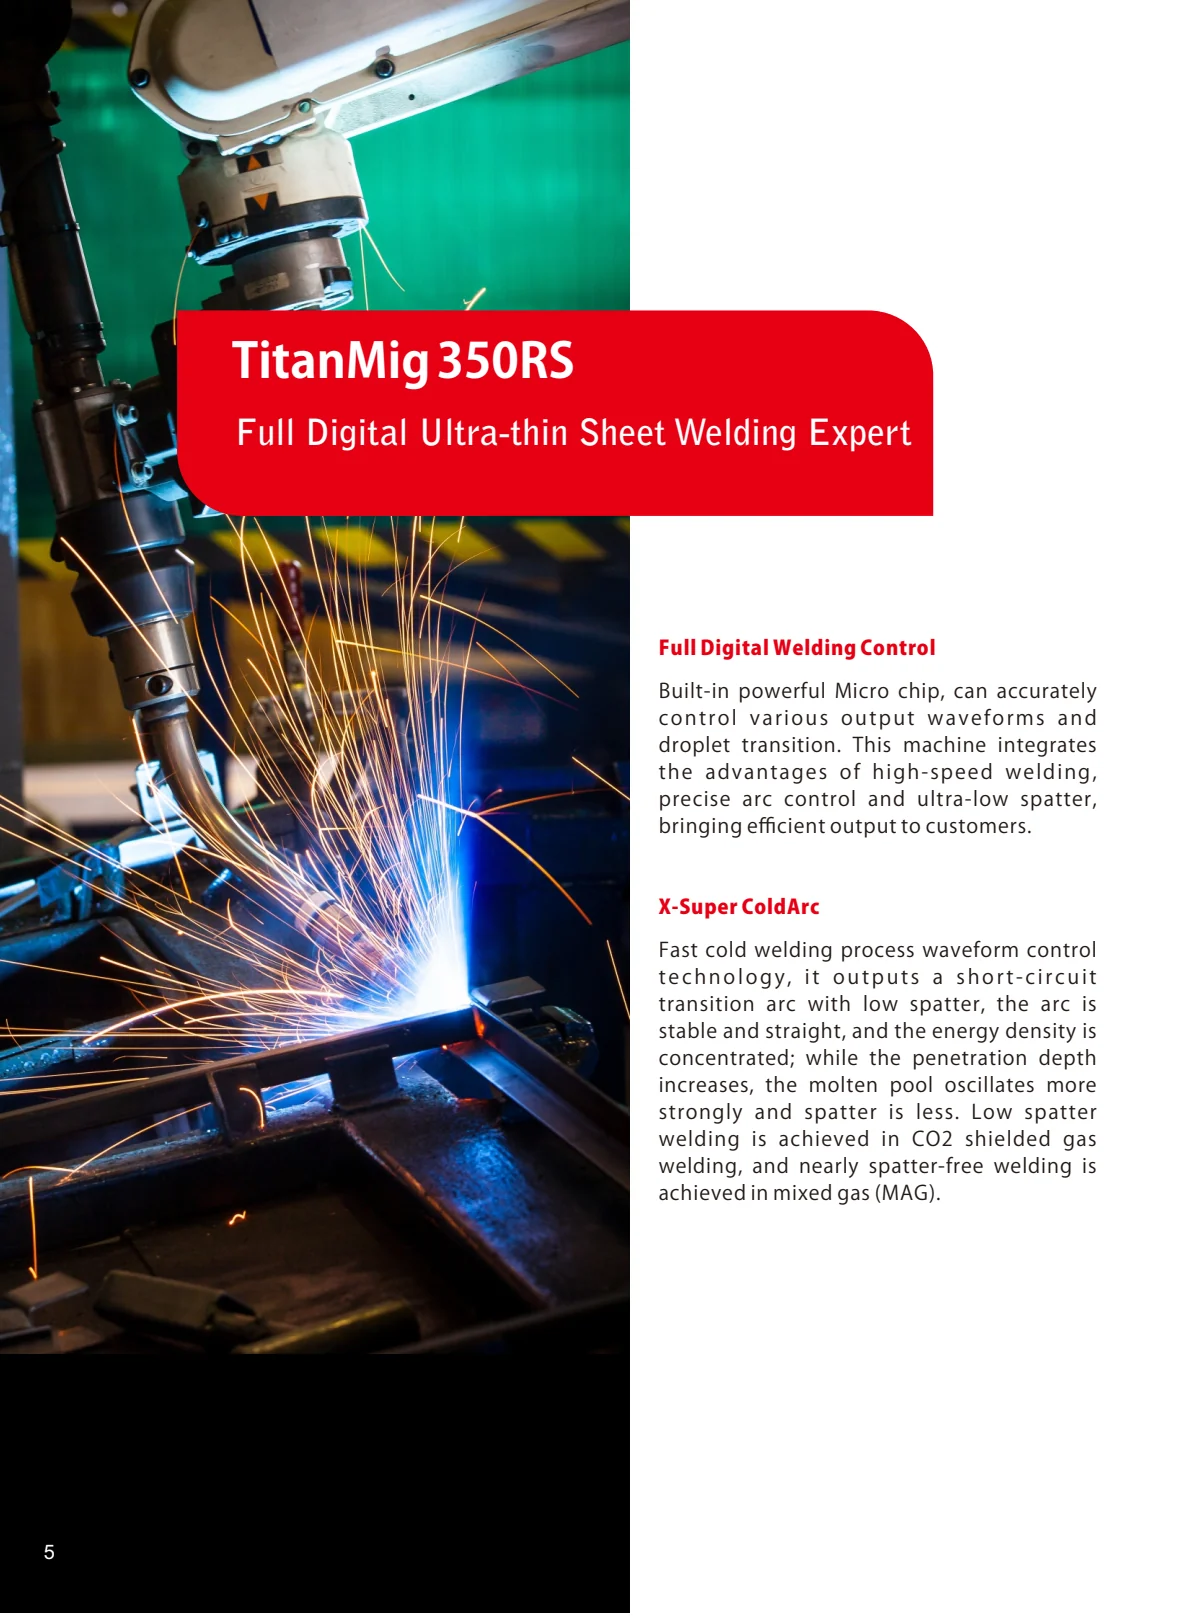
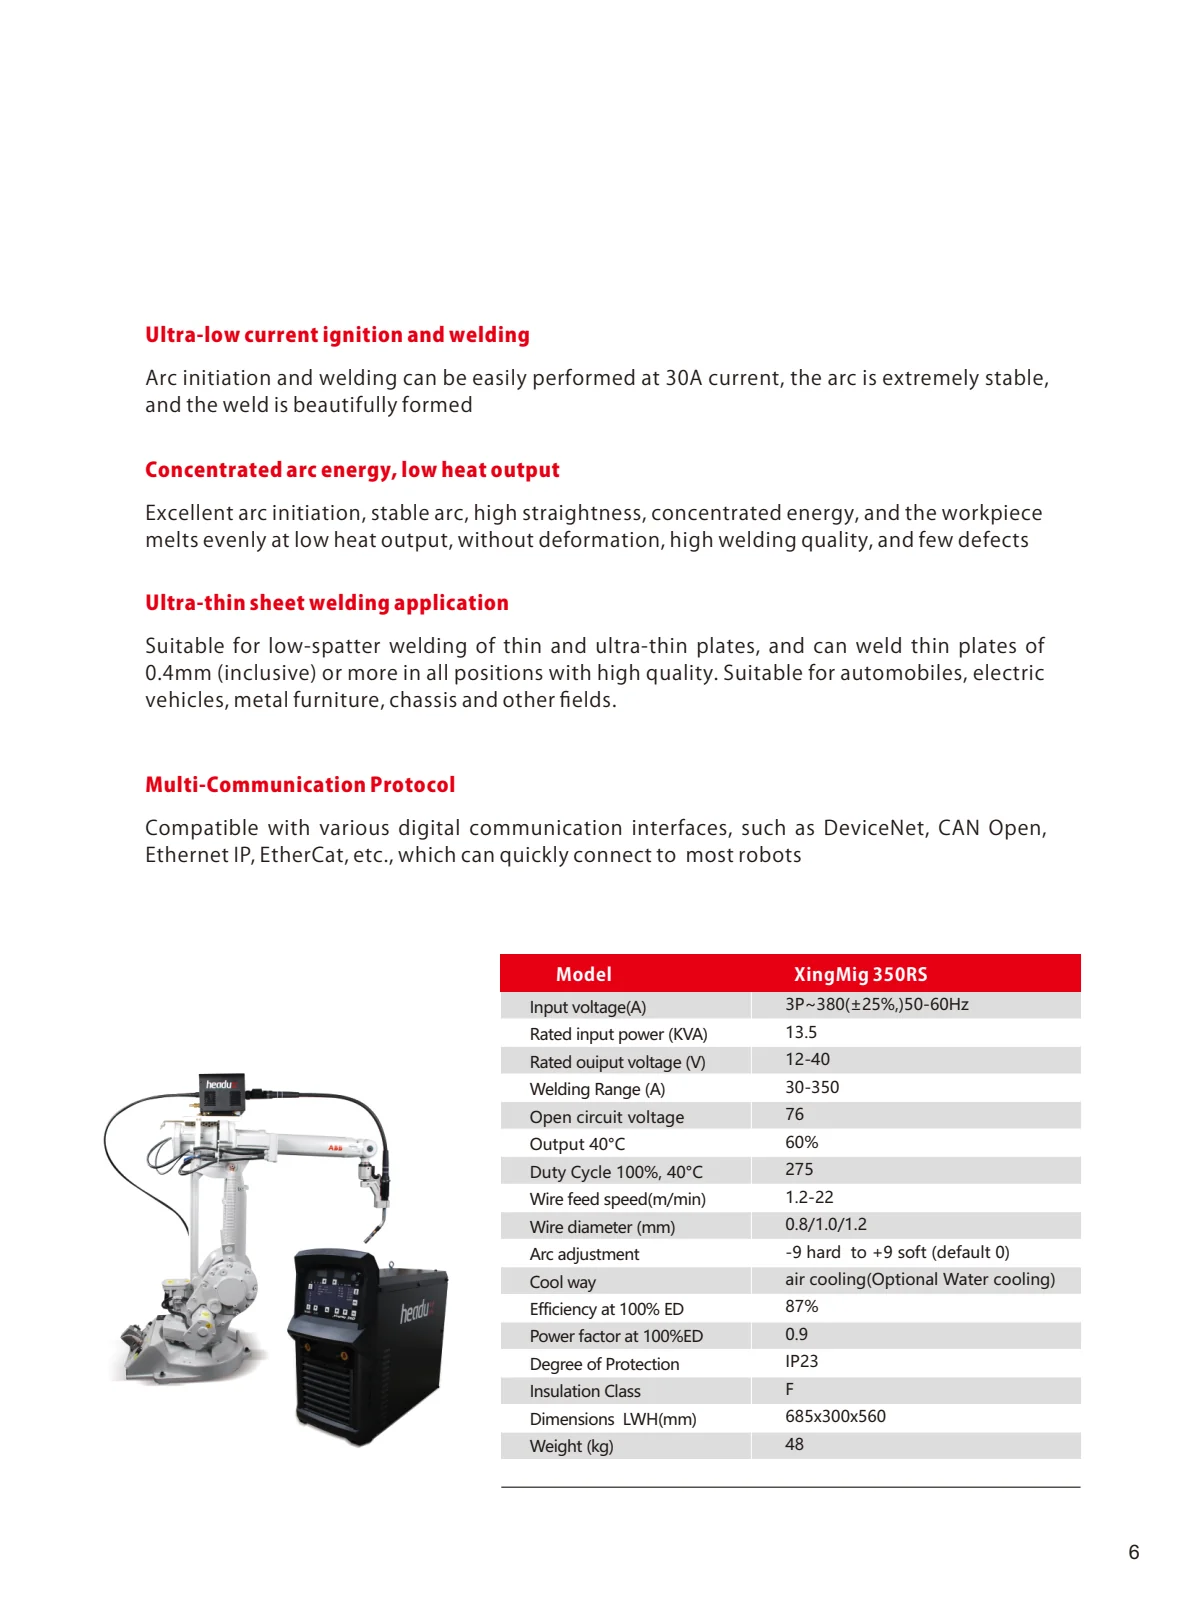
Full Digital Welding Control Built-in powerful Micro chip, can accurately c o n t r o l v a r i o u s o u t p u t w a v e f o r m s a n d droplet transition. This machine integrates t h e a d v a n t a g e s o f h i g h - s p e e d w e l d i n g , precise arc control and ultra-low spatter, bringing efficient output to customers. X-Super ColdArc Fast cold welding process waveform control t e c h n o l o g y , i t o u t p u t s a s h o r t - c i r c u i t transition arc with low spatter, the arc is stable and straight, and the energy density is concentrated; while the penetration depth increases, the molten pool oscillates more strongly and spatter is less. Low spatter welding is achieved in CO2 shielded gas welding, and nearly spatter-free welding is achieved in mixed gas (MAG). 5 6 TitanMig 350RS Full Digital Ultra-thin Sheet Welding Expert Concentrated arc energy, low heat output Excellent arc initiation, stable arc, high straightness, concentrated energy, and the workpiece melts evenly at low heat output, without deformation, high welding quality, and few defects Ultra-thin sheet welding application Suitable for low-spatter welding of thin and ultra-thin plates, and can weld thin plates of 0.4mm (inclusive) or more in all positions with high quality. Suitable for automobiles, electric vehicles, metal furniture, chassis and other fields. Multi-Communication Protocol Compatible with various digital communication interfaces, such as DeviceNet, CAN Open, Ethernet IP, EtherCat, etc., which can quickly connect to most robots Ultra-low current ignition and welding Arc initiation and welding can be easily performed at 30A current, the arc is extremely stable, and the weld is beautifully formed 3P~380(±25%,)50-60Hz 13.5 12-40 30-350 76 60% 275 1.2-22 0.8/1.0/1.2 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 48 Input voltage(A) Rated input power (KVA) Rated ouiput voltage (V) Welding Range (A) Open circuit voltage Output 40°C Duty Cycle 100%, 40°C Wire feed speed(m/min) Wire diameter (mm) Arc adjustment Cool way Efficiency at 100% ED Power factor at 100%ED Degree of Protection Insulation Class Dimensions LWH(mm) Weight (kg) Model XingMig 350RS
Read page text
Full Digital Welding Control Built-in powerful Micro chip, can accurately c o n t r o l v a r i o u s o u t p u t w a v e f o r m s a n d droplet transition. This machine integrates t h e a d v a n t a g e s o f h i g h - s p e e d w e l d i n g , precise arc control and ultra-low spatter, bringing efficient output to customers. X-Super ColdArc Fast cold welding process waveform control t e c h n o l o g y , i t o u t p u t s a s h o r t - c i r c u i t transition arc with low spatter, the arc is stable and straight, and the energy density is concentrated; while the penetration depth increases, the molten pool oscillates more strongly and spatter is less. Low spatter welding is achieved in CO2 shielded gas welding, and nearly spatter-free welding is achieved in mixed gas (MAG). 5 6 TitanMig 350RS Full Digital Ultra-thin Sheet Welding Expert Concentrated arc energy, low heat output Excellent arc initiation, stable arc, high straightness, concentrated energy, and the workpiece melts evenly at low heat output, without deformation, high welding quality, and few defects Ultra-thin sheet welding application Suitable for low-spatter welding of thin and ultra-thin plates, and can weld thin plates of 0.4mm (inclusive) or more in all positions with high quality. Suitable for automobiles, electric vehicles, metal furniture, chassis and other fields. Multi-Communication Protocol Compatible with various digital communication interfaces, such as DeviceNet, CAN Open, Ethernet IP, EtherCat, etc., which can quickly connect to most robots Ultra-low current ignition and welding Arc initiation and welding can be easily performed at 30A current, the arc is extremely stable, and the weld is beautifully formed 3P~380(±25%,)50-60Hz 13.5 12-40 30-350 76 60% 275 1.2-22 0.8/1.0/1.2 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 48 Input voltage(A) Rated input power (KVA) Rated ouiput voltage (V) Welding Range (A) Open circuit voltage Output 40°C Duty Cycle 100%, 40°C Wire feed speed(m/min) Wire diameter (mm) Arc adjustment Cool way Efficiency at 100% ED Power factor at 100%ED Degree of Protection Insulation Class Dimensions LWH(mm) Weight (kg) Model XingMig 350RS
Read page text
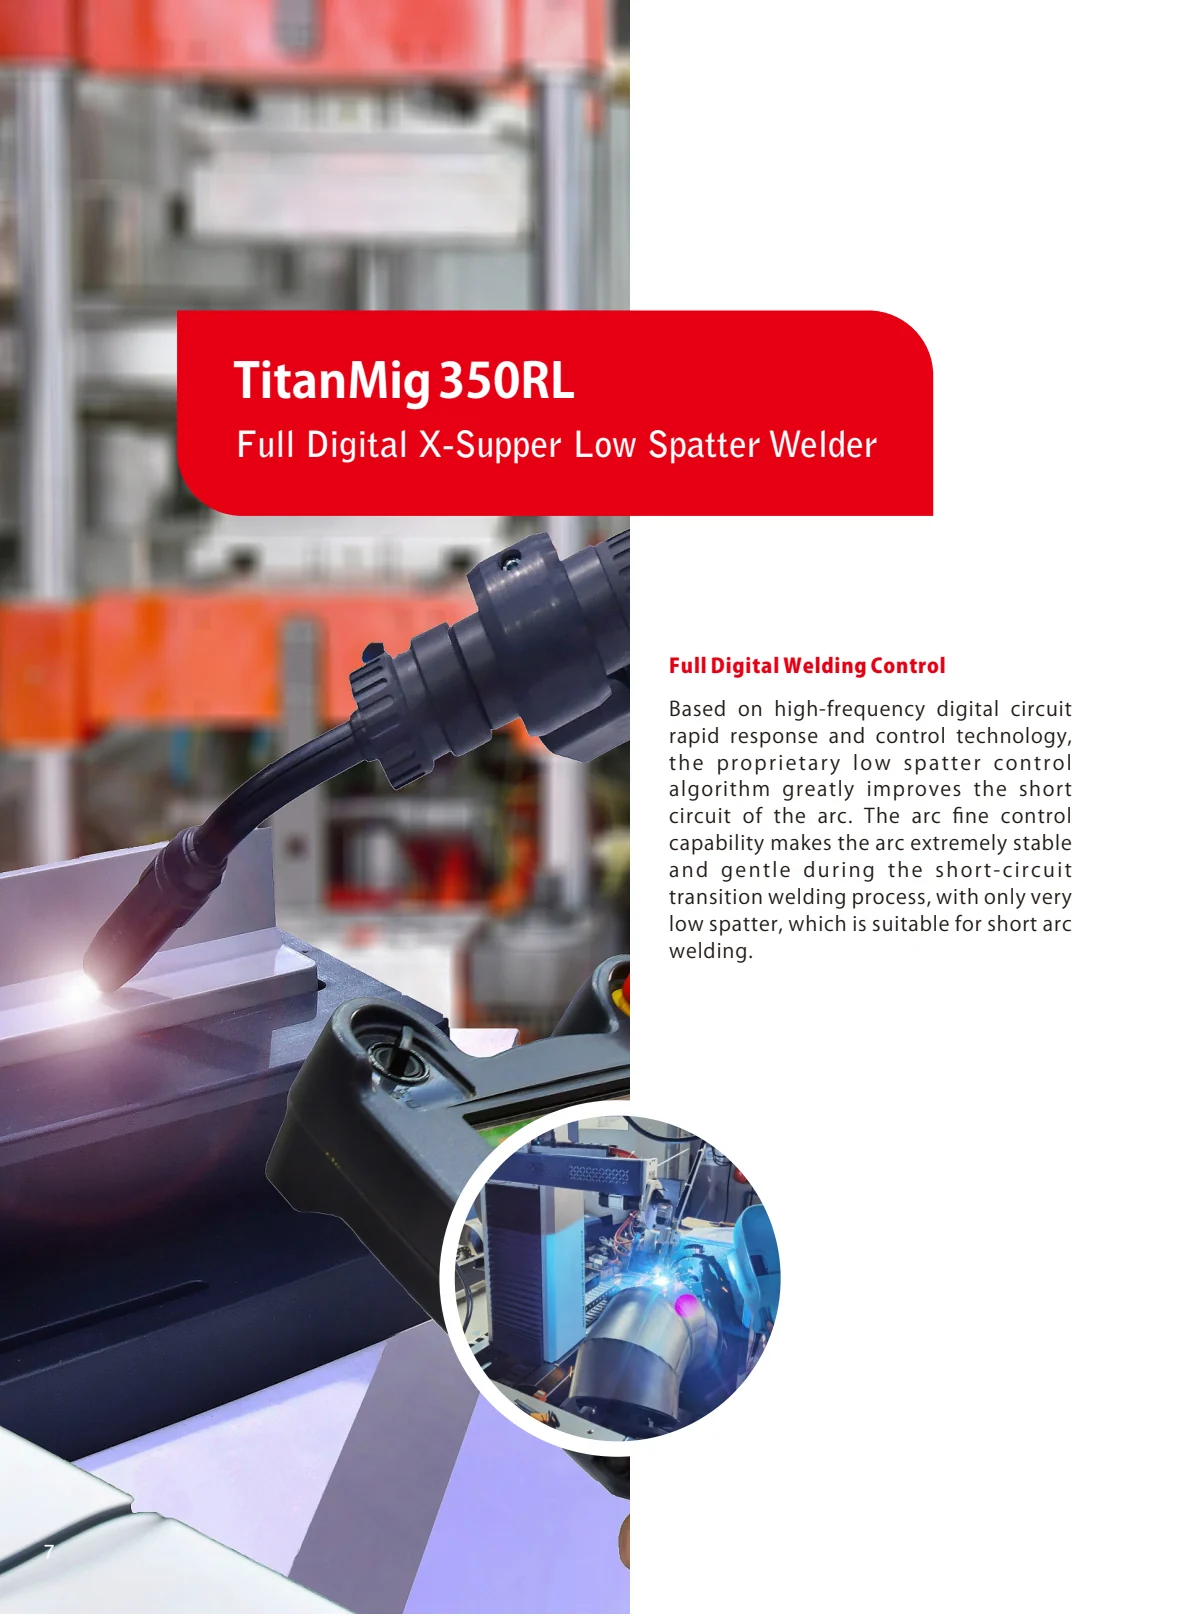
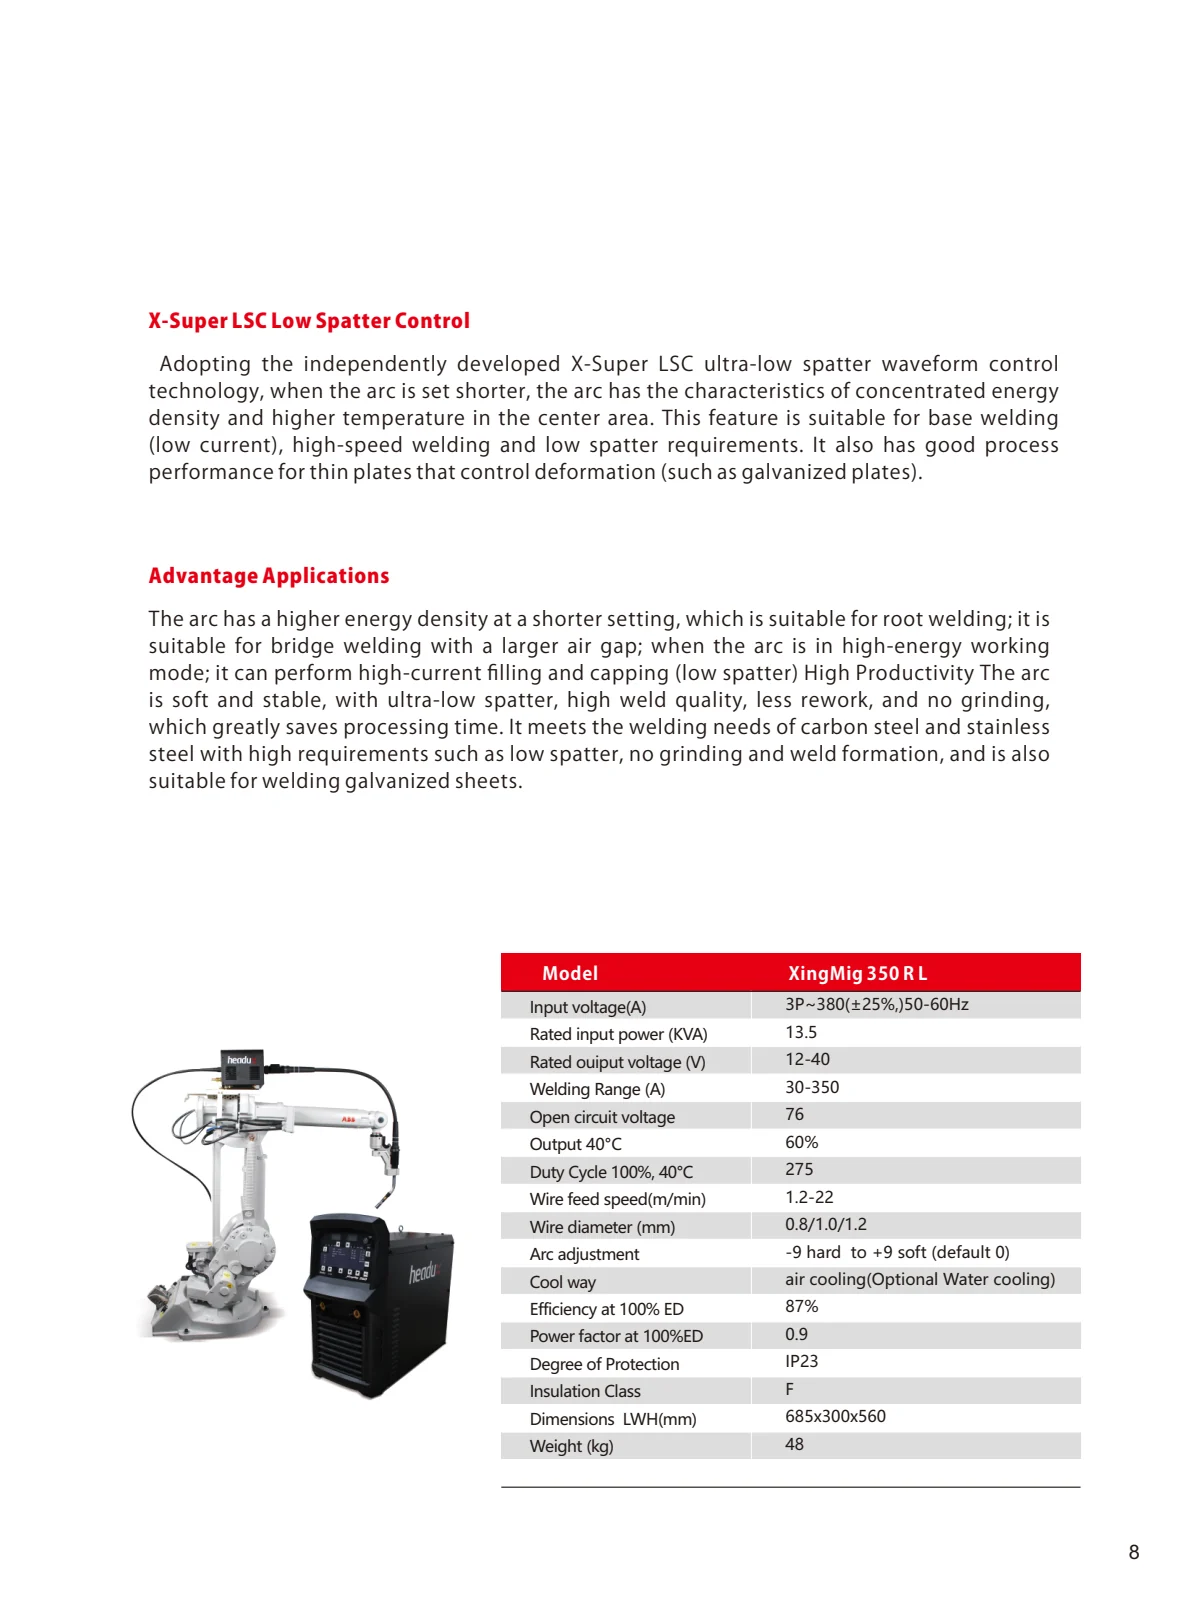
Full Digital X-Supper Low Spatter Welder Full Digital Welding Control Based on high-frequency digital circuit rapid response and control technology, t h e p r o p r i e t a r y l o w s p a t t e r c o n t r o l algorithm greatly improves the short circuit of the arc. The arc fine control capability makes the arc extremely stable a n d g e n t l e d u r i n g t h e s h o r t - c i r c u i t transition welding process, with only very low spatter, which is suitable for short arc welding. X-Super LSC Low Spatter Control Adopting the independently developed X-Super LSC ultra-low spatter waveform control technology, when the arc is set shorter, the arc has the characteristics of concentrated energy density and higher temperature in the center area. This feature is suitable for base welding (low current), high-speed welding and low spatter requirements. It also has good process performance for thin plates that control deformation (such as galvanized plates). TitanMig 350RL Model XingMig 350 R L 7 8 Advantage Applications The arc has a higher energy density at a shorter setting, which is suitable for root welding; it is suitable for bridge welding with a larger air gap; when the arc is in high-energy working mode; it can perform high-current filling and capping (low spatter) High Productivity The arc is soft and stable, with ultra-low spatter, high weld quality, less rework, and no grinding, which greatly saves processing time. It meets the welding needs of carbon steel and stainless steel with high requirements such as low spatter, no grinding and weld formation, and is also suitable for welding galvanized sheets. 3P~380(±25%,)50-60Hz 13.5 12-40 30-350 76 60% 275 1.2-22 0.8/1.0/1.2 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 48 Input voltage(A) Rated input power (KVA) Rated ouiput voltage (V) Welding Range (A) Open circuit voltage Output 40°C Duty Cycle 100%, 40°C Wire feed speed(m/min) Wire diameter (mm) Arc adjustment Cool way Efficiency at 100% ED Power factor at 100%ED Degree of Protection Insulation Class Dimensions LWH(mm) Weight (kg)
Read page text
Full Digital X-Supper Low Spatter Welder Full Digital Welding Control Based on high-frequency digital circuit rapid response and control technology, t h e p r o p r i e t a r y l o w s p a t t e r c o n t r o l algorithm greatly improves the short circuit of the arc. The arc fine control capability makes the arc extremely stable a n d g e n t l e d u r i n g t h e s h o r t - c i r c u i t transition welding process, with only very low spatter, which is suitable for short arc welding. X-Super LSC Low Spatter Control Adopting the independently developed X-Super LSC ultra-low spatter waveform control technology, when the arc is set shorter, the arc has the characteristics of concentrated energy density and higher temperature in the center area. This feature is suitable for base welding (low current), high-speed welding and low spatter requirements. It also has good process performance for thin plates that control deformation (such as galvanized plates). TitanMig 350RL Model XingMig 350 R L 7 8 Advantage Applications The arc has a higher energy density at a shorter setting, which is suitable for root welding; it is suitable for bridge welding with a larger air gap; when the arc is in high-energy working mode; it can perform high-current filling and capping (low spatter) High Productivity The arc is soft and stable, with ultra-low spatter, high weld quality, less rework, and no grinding, which greatly saves processing time. It meets the welding needs of carbon steel and stainless steel with high requirements such as low spatter, no grinding and weld formation, and is also suitable for welding galvanized sheets. 3P~380(±25%,)50-60Hz 13.5 12-40 30-350 76 60% 275 1.2-22 0.8/1.0/1.2 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 48 Input voltage(A) Rated input power (KVA) Rated ouiput voltage (V) Welding Range (A) Open circuit voltage Output 40°C Duty Cycle 100%, 40°C Wire feed speed(m/min) Wire diameter (mm) Arc adjustment Cool way Efficiency at 100% ED Power factor at 100%ED Degree of Protection Insulation Class Dimensions LWH(mm) Weight (kg)
Read page text
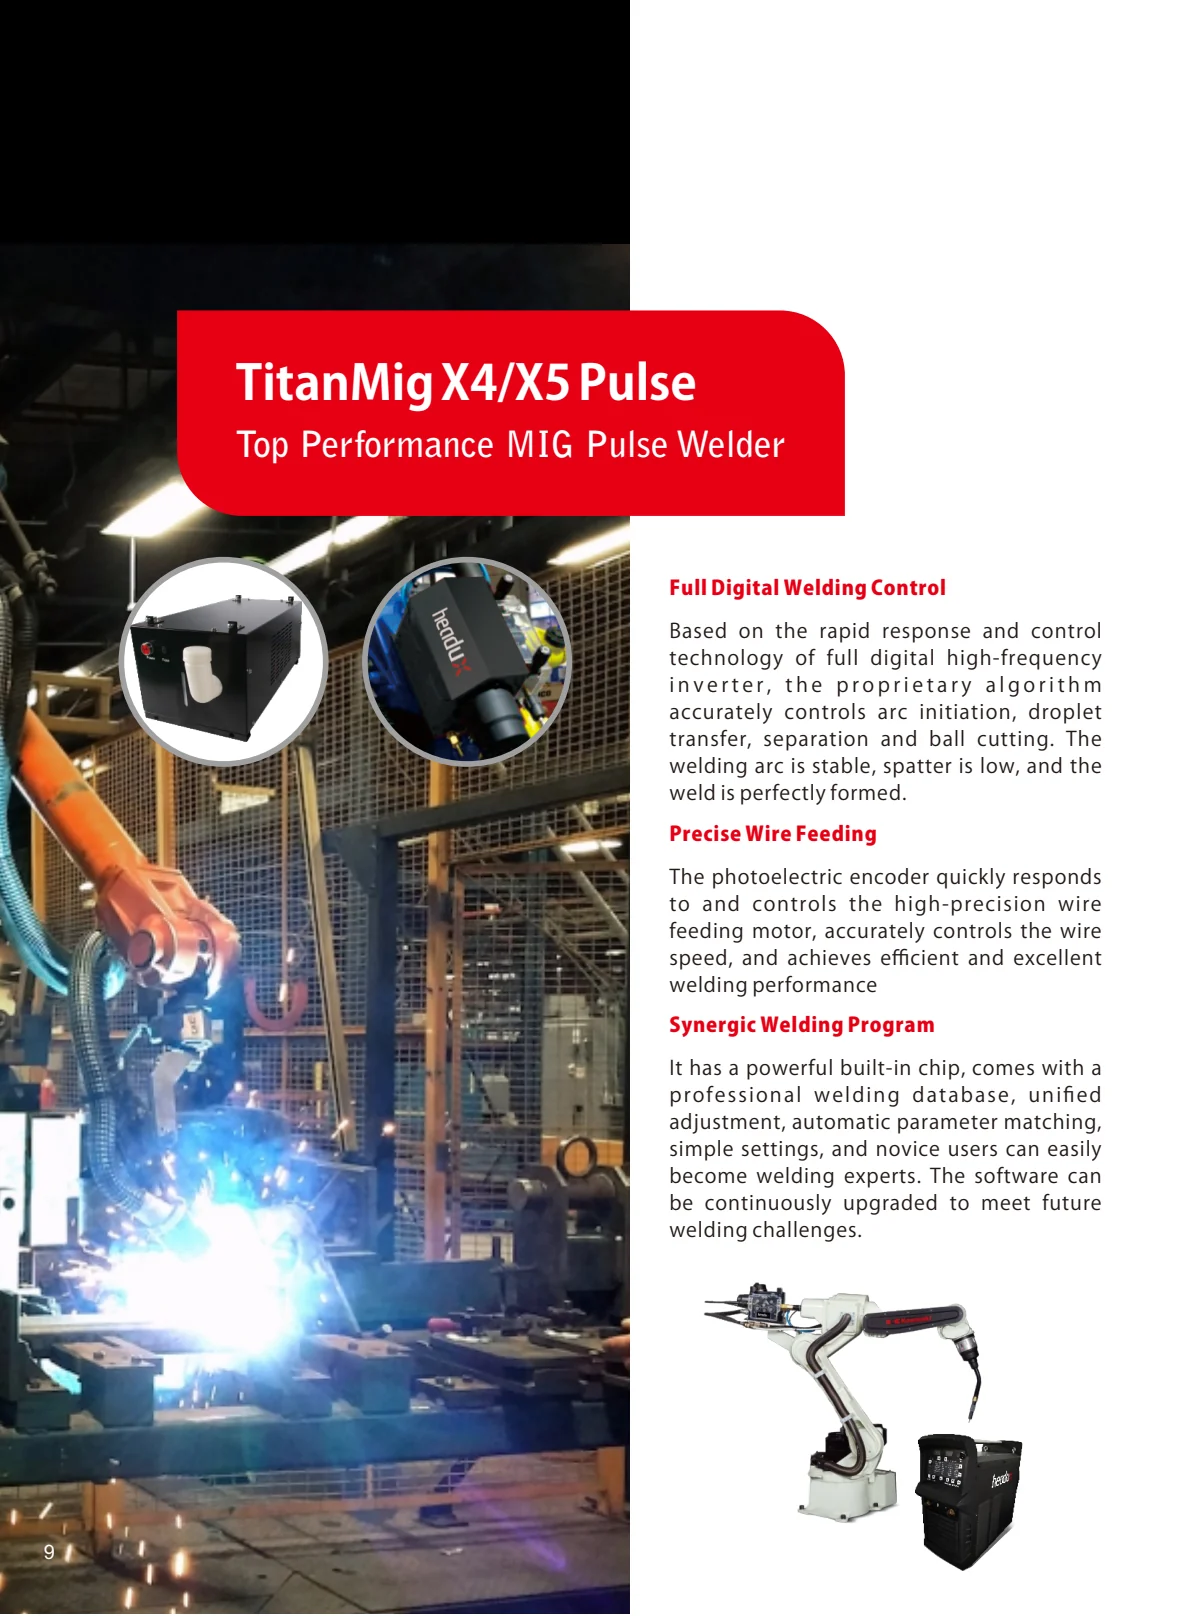
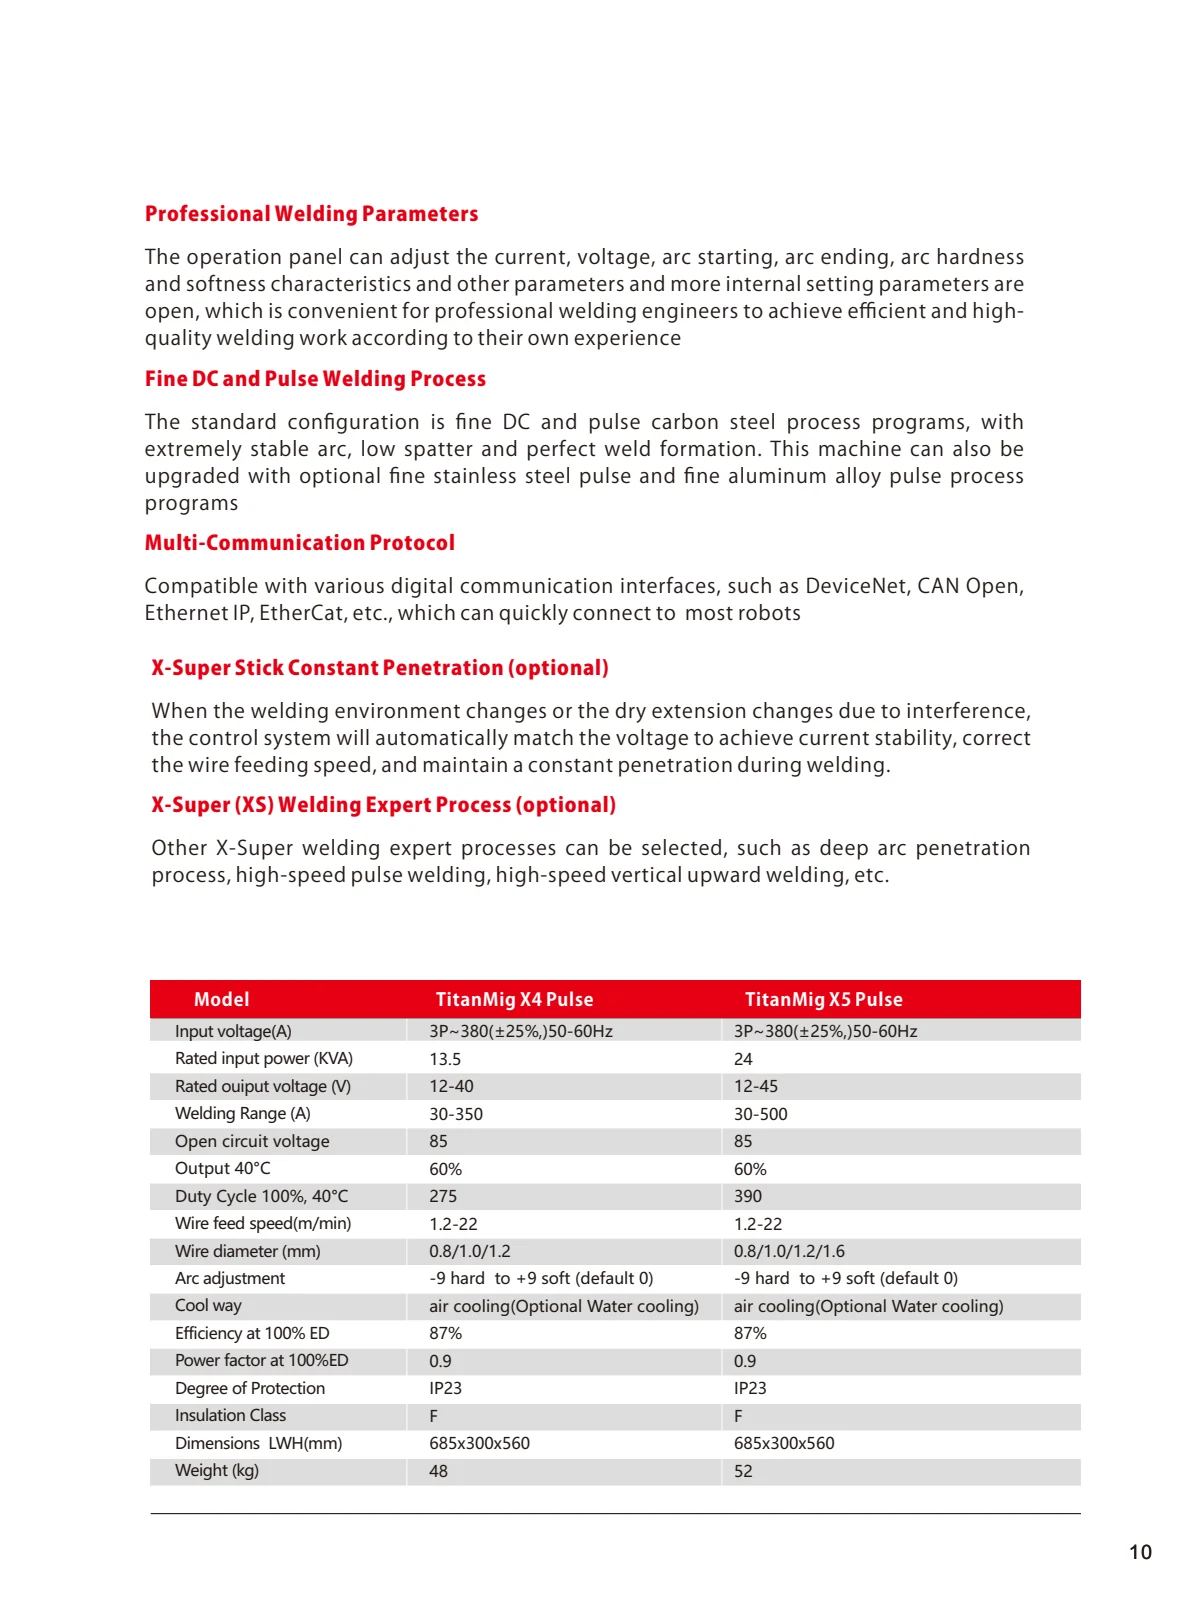
Top Performance MIG Pulse Welder 109 10 Full Digital Welding Control Based on the rapid response and control technology of full digital high-frequency i n v e r t e r , t h e p r o p r i e t a r y a l g o r i t h m accurately controls arc initiation, droplet transfer, separation and ball cutting. The welding arc is stable, spatter is low, and the weld is perfectly formed. Precise Wire Feeding The photoelectric encoder quickly responds to and controls the high-precision wire feeding motor, accurately controls the wire speed, and achieves efficient and excellent welding performance Synergic Welding Program It has a powerful built-in chip, comes with a p r o f e s s i o n a l w e l d i n g d a t a b a s e , u n i fi e d adjustment, automatic parameter matching, simple settings, and novice users can easily become welding experts. The software can be continuously upgraded to meet future welding challenges. X-Super Stick Constant Penetration (optional) When the welding environment changes or the dry extension changes due to interference, the control system will automatically match the voltage to achieve current stability, correct the wire feeding speed, and maintain a constant penetration during welding. X-Super (XS) Welding Expert Process (optional) Other X-Super welding expert processes can be selected, such as deep arc penetration process, high-speed pulse welding, high-speed vertical upward welding, etc. 10 TitanMig X4 R TitanMig X5 R 3P~380(±25%,)50-60Hz 13.5 12-40 30-350 85 60% 275 1.2-22 0.8/1.0/1.2 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 48 3P~380(±25%,)50-60Hz 24 12-45 30-500 85 60% 390 1.2-22 0.8/1.0/1.2/1.6 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 52 TitanMig X4/X5 Pulse Model TitanMig X4 Pulse TitanMig X5 Pulse Professional Welding Parameters The operation panel can adjust the current, voltage, arc starting, arc ending, arc hardness and softness characteristics and other parameters and more internal setting parameters are open, which is convenient for professional welding engineers to achieve efficient and high- quality welding work according to their own experience Fine DC and Pulse Welding Process The standard configuration is fine DC and pulse carbon steel process programs, with extremely stable arc, low spatter and perfect weld formation. This machine can also be upgraded with optional fine stainless steel pulse and fine aluminum alloy pulse process programs Multi-Communication Protocol Compatible with various digital communication interfaces, such as DeviceNet, CAN Open, Ethernet IP, EtherCat, etc., which can quickly connect to most robots Input voltage(A) Rated input power (KVA) Rated ouiput voltage (V) Welding Range (A) Open circuit voltage Output 40°C Duty Cycle 100%, 40°C Wire feed speed(m/min) Wire diameter (mm) Arc adjustment Cool way Efficiency at 100% ED Power factor at 100%ED Degree of Protection Insulation Class Dimensions LWH(mm) Weight (kg)
Read page text
Top Performance MIG Pulse Welder 109 10 Full Digital Welding Control Based on the rapid response and control technology of full digital high-frequency i n v e r t e r , t h e p r o p r i e t a r y a l g o r i t h m accurately controls arc initiation, droplet transfer, separation and ball cutting. The welding arc is stable, spatter is low, and the weld is perfectly formed. Precise Wire Feeding The photoelectric encoder quickly responds to and controls the high-precision wire feeding motor, accurately controls the wire speed, and achieves efficient and excellent welding performance Synergic Welding Program It has a powerful built-in chip, comes with a p r o f e s s i o n a l w e l d i n g d a t a b a s e , u n i fi e d adjustment, automatic parameter matching, simple settings, and novice users can easily become welding experts. The software can be continuously upgraded to meet future welding challenges. X-Super Stick Constant Penetration (optional) When the welding environment changes or the dry extension changes due to interference, the control system will automatically match the voltage to achieve current stability, correct the wire feeding speed, and maintain a constant penetration during welding. X-Super (XS) Welding Expert Process (optional) Other X-Super welding expert processes can be selected, such as deep arc penetration process, high-speed pulse welding, high-speed vertical upward welding, etc. 10 TitanMig X4 R TitanMig X5 R 3P~380(±25%,)50-60Hz 13.5 12-40 30-350 85 60% 275 1.2-22 0.8/1.0/1.2 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 48 3P~380(±25%,)50-60Hz 24 12-45 30-500 85 60% 390 1.2-22 0.8/1.0/1.2/1.6 -9 hard to +9 soft (default 0) air cooling(Optional Water cooling) 87% 0.9 IP23 F 685x300x560 52 TitanMig X4/X5 Pulse Model TitanMig X4 Pulse TitanMig X5 Pulse Professional Welding Parameters The operation panel can adjust the current, voltage, arc starting, arc ending, arc hardness and softness characteristics and other parameters and more internal setting parameters are open, which is convenient for professional welding engineers to achieve efficient and high- quality welding work according to their own experience Fine DC and Pulse Welding Process The standard configuration is fine DC and pulse carbon steel process programs, with extremely stable arc, low spatter and perfect weld formation. This machine can also be upgraded with optional fine stainless steel pulse and fine aluminum alloy pulse process programs Multi-Communication Protocol Compatible with various digital communication interfaces, such as DeviceNet, CAN Open, Ethernet IP, EtherCat, etc., which can quickly connect to most robots Input voltage(A) Rated input power (KVA) Rated ouiput voltage (V) Welding Range (A) Open circuit voltage Output 40°C Duty Cycle 100%, 40°C Wire feed speed(m/min) Wire diameter (mm) Arc adjustment Cool way Efficiency at 100% ED Power factor at 100%ED Degree of Protection Insulation Class Dimensions LWH(mm) Weight (kg)
Read page text
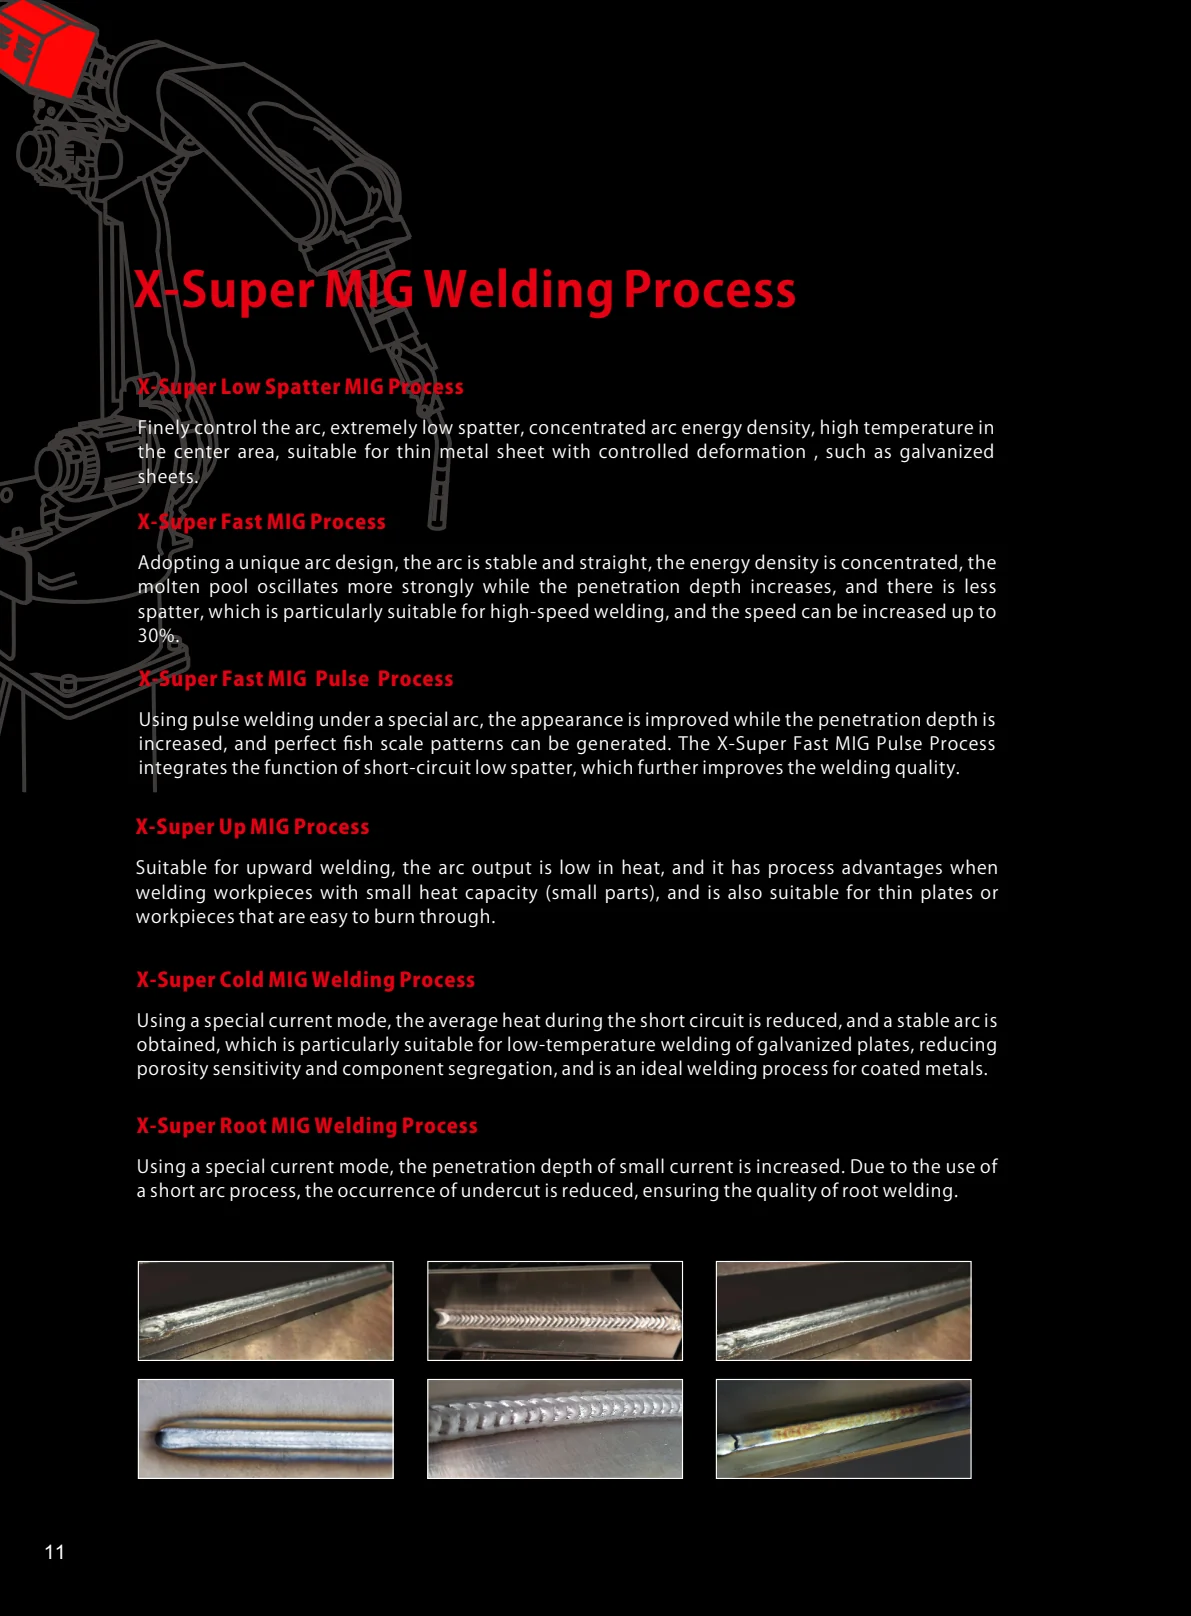
X-Super Low Spatter MIG Process Finely control the arc, extremely low spatter, concentrated arc energy density, high temperature in the center area, suitable for thin metal sheet with controlled deformation , such as galvanized sheets. X-Super Fast MIG Process Adopting a unique arc design, the arc is stable and straight, the energy density is concentrated, the molten pool oscillates more strongly while the penetration depth increases, and there is less spatter, which is particularly suitable for high-speed welding, and the speed can be increased up to 30%. X-Super Cold MIG Welding Process Using a special current mode, the average heat during the short circuit is reduced, and a stable arc is obtained, which is particularly suitable for low-temperature welding of galvanized plates, reducing porosity sensitivity and component segregation, and is an ideal welding process for coated metals. X-Super Root MIG Welding Process Using a special current mode, the penetration depth of small current is increased. Due to the use of a short arc process, the occurrence of undercut is reduced, ensuring the quality of root welding. 11 X-Super MIG Welding Process X-Super Fast MIG Pulse Process Using pulse welding under a special arc, the appearance is improved while the penetration depth is increased, and perfect fish scale patterns can be generated. The X-Super Fast MIG Pulse Process integrates the function of short-circuit low spatter, which further improves the welding quality. X-Super Up MIG Process Suitable for upward welding, the arc output is low in heat, and it has process advantages when welding workpieces with small heat capacity (small parts), and is also suitable for thin plates or workpieces that are easy to burn through.
Read page text
X-Super Low Spatter MIG Process Finely control the arc, extremely low spatter, concentrated arc energy density, high temperature in the center area, suitable for thin metal sheet with controlled deformation , such as galvanized sheets. X-Super Fast MIG Process Adopting a unique arc design, the arc is stable and straight, the energy density is concentrated, the molten pool oscillates more strongly while the penetration depth increases, and there is less spatter, which is particularly suitable for high-speed welding, and the speed can be increased up to 30%. X-Super Cold MIG Welding Process Using a special current mode, the average heat during the short circuit is reduced, and a stable arc is obtained, which is particularly suitable for low-temperature welding of galvanized plates, reducing porosity sensitivity and component segregation, and is an ideal welding process for coated metals. X-Super Root MIG Welding Process Using a special current mode, the penetration depth of small current is increased. Due to the use of a short arc process, the occurrence of undercut is reduced, ensuring the quality of root welding. 11 X-Super MIG Welding Process X-Super Fast MIG Pulse Process Using pulse welding under a special arc, the appearance is improved while the penetration depth is increased, and perfect fish scale patterns can be generated. The X-Super Fast MIG Pulse Process integrates the function of short-circuit low spatter, which further improves the welding quality. X-Super Up MIG Process Suitable for upward welding, the arc output is low in heat, and it has process advantages when welding workpieces with small heat capacity (small parts), and is also suitable for thin plates or workpieces that are easy to burn through.
Read page text
Headux International GmbH Max-Planck-Str. 34, 50858 Cologne , Germany. EUROPE ASIA & PACIFIC Headux Electric Co., Ltd. Fl. 8, Bldg A1, Youlitong Industrial Park, 56 Qingsong Rd., Pingshan, 518111 Shenzhen,China. Email:[email protected] Http://www.headux.com